


Top 10 packing conveyor Manufacturers in the world
Dec 10, 2025
Leave a message
Introduction to Packing Conveyors
Packing conveyors are essential equipment in various industries, playing a crucial role in the packaging process. They are designed to transport products from one point to another within a packaging line, ensuring a smooth and efficient flow of goods. These conveyors can handle a wide range of products, from small items like pills and candies to large and heavy packages. They come in different types, such as belt conveyors, roller conveyors, chain conveyors, and screw conveyors, each with its own unique features and applications. The use of packing conveyors not only improves productivity but also reduces labor costs and minimizes the risk of product damage during the packaging process.
Top 10 Manufacturers
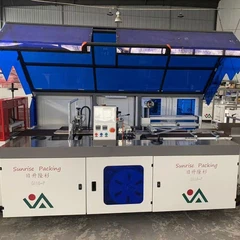
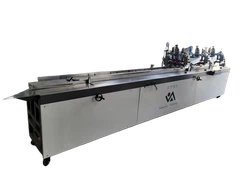
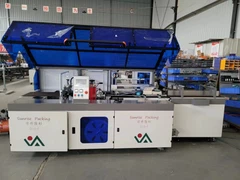
1. Sunrise (Tianjin) Packaging Machinery Co., Ltd.
Sunrise (Tianjin) Packaging Machinery Co., Ltd. is a leading manufacturer of packaging machinery, including packing conveyors, based in Tianjin, China. The company has been dedicated to the research, development, production, and sales of packaging equipment for many years. With a team of professional engineers and technicians, Sunrise is committed to providing high - quality, reliable, and innovative packaging solutions to customers around the world.
Features in Packing Conveyors:
- Customization: Sunrise offers highly customizable packing conveyors. They can design conveyors according to the specific requirements of different industries, such as the size, weight, and shape of the products to be transported. For example, in the food industry, where hygiene is of utmost importance, they can provide conveyors with special food - grade belts and easy - to - clean structures.
- Advanced Technology: The company incorporates advanced technology into its conveyors. Their conveyors are equipped with intelligent control systems that can adjust the speed, direction, and operation mode according to the production needs. This not only improves the efficiency of the packaging line but also reduces energy consumption.
- High - Quality Materials: Sunrise uses high - quality materials in the manufacturing of its conveyors. The frames are made of strong and durable steel, and the belts are selected for their wear - resistance and anti - static properties. This ensures the long - term reliable operation of the conveyors.
Advantages:
- Cost - effectiveness: Compared with some international brands, Sunrise offers cost - effective packing conveyors without sacrificing quality. This makes it an attractive choice for small and medium - sized enterprises that are looking for reliable packaging solutions within a limited budget.
- Excellent After - sales Service: The company provides comprehensive after - sales service, including installation, debugging, maintenance, and technical support. Their service team can respond quickly to customers' needs, ensuring minimal downtime in case of any problems with the conveyors.
- Global Reach: Sunrise has established a wide sales network around the world. They have exported their products to many countries and regions, and have received positive feedback from customers. Their website, https://www.tjrslspackingmachine.com/, provides detailed information about their products and services, making it easy for customers to contact them.
2. Dematic
Dematic is a global leader in providing integrated automated material handling solutions, including packing conveyors. With a history dating back over 200 years, the company has a wealth of experience in the industry. Dematic operates in more than 25 countries and has a large customer base across various sectors, such as e - commerce, retail, and manufacturing.
Features in Packing Conveyors:
- Automation and Integration: Dematic's packing conveyors are highly automated and can be seamlessly integrated into complex material handling systems. They can work in conjunction with other equipment such as robotic pickers, sorters, and storage systems to create a fully automated packaging line. For example, in a large - scale e - commerce fulfillment center, Dematic's conveyors can transport products from the storage area to the packing stations, and then to the shipping area, all with minimal human intervention.
- High - Speed Operation: The company's conveyors are designed for high - speed operation. They can achieve very high throughput rates, which is crucial for industries with high - volume production requirements. Dematic uses advanced drive systems and control technologies to ensure smooth and stable high - speed operation of the conveyors.
- Flexibility: Dematic's packing conveyors are highly flexible. They can be easily reconfigured and adapted to different production layouts and requirements. This is especially useful for companies that need to change their packaging processes frequently due to product changes or market demands.
Advantages:
- Innovative Technology: Dematic invests heavily in research and development, constantly introducing new and innovative technologies in its packing conveyors. Their solutions are at the forefront of the industry, helping customers to improve their competitiveness.
- Global Support: With its global presence, Dematic can provide comprehensive support to its customers around the world. They have local service teams in different countries, which can provide timely maintenance and technical support to ensure the smooth operation of the conveyors.
- Proven Track Record: Dematic has a long - standing reputation for delivering high - quality and reliable material handling solutions. Their packing conveyors have been widely used in many large - scale projects, and have proven to be effective in improving productivity and reducing costs.
3. Intelligrated (now part of Honeywell)
Intelligrated, now a part of Honeywell, is a well - known provider of automated material handling solutions, including packing conveyors. The company has a strong focus on innovation and technology, and has developed a range of advanced conveyor systems for various industries.
Features in Packing Conveyors:
- Smart Conveyor Technology: Intelligrated's packing conveyors are equipped with smart technology. They use sensors and advanced control algorithms to monitor the operation of the conveyors in real - time. This allows for proactive maintenance, as the system can detect potential problems before they cause breakdowns. For example, the sensors can detect abnormal vibrations or temperature changes in the conveyor components, and send alerts to the maintenance team.
- Energy - Efficient Design: The company pays great attention to energy efficiency in the design of its conveyors. They use energy - saving motors and advanced control systems to reduce power consumption. In addition, their conveyors are designed to minimize friction and waste, further improving energy efficiency.
- Modular Design: Intelligrated's packing conveyors have a modular design, which makes them easy to install, expand, and modify. The modular components can be easily assembled and disassembled, allowing for quick reconfiguration of the conveyor system according to the changing production needs.
Advantages:
- Honeywell's Resources: As a part of Honeywell, Intelligrated can leverage Honeywell's extensive resources in research, development, and global support. This enables them to offer more advanced and reliable packing conveyor solutions to their customers.
- Industry - Specific Solutions: Intelligrated has in - depth knowledge of different industries and can provide industry - specific packing conveyor solutions. For example, in the food and beverage industry, they can design conveyors that meet the strict hygiene and safety requirements.
- System Integration Expertise: The company has strong system integration expertise. They can integrate their packing conveyors with other equipment and software systems to create a complete and efficient material handling solution.
4. Bosch Rexroth
Bosch Rexroth is a leading global supplier of drive and control technologies, and also offers high - quality packing conveyors. The company has a long history of innovation and is known for its precision engineering and reliable products.
Features in Packing Conveyors:
- Precision Engineering: Bosch Rexroth's packing conveyors are engineered with high precision. They offer accurate positioning and smooth movement of products, which is crucial for the packaging process. The company uses advanced manufacturing techniques and high - quality components to ensure the precision and reliability of the conveyors.
- Compact Design: The conveyors are designed to be compact, which is beneficial for companies with limited floor space. Bosch Rexroth can design conveyors that can fit into tight spaces without sacrificing performance. This is especially useful for small - scale manufacturing facilities or warehouses.
- High - Performance Drive Systems: The company uses high - performance drive systems in its packing conveyors. These drive systems can provide high torque and smooth acceleration, allowing the conveyors to handle heavy loads and operate at high speeds.
Advantages:
- Global Brand Reputation: Bosch Rexroth is a well - known global brand with a reputation for quality and reliability. Customers can have confidence in the performance and durability of their packing conveyors.
- Comprehensive Product Portfolio: The company offers a comprehensive product portfolio of packing conveyors, including different types and sizes to meet the diverse needs of customers. They also provide a range of accessories and options for the conveyors, allowing customers to customize their systems.
- Technical Support: Bosch Rexroth provides excellent technical support to its customers. Their team of experts can offer advice on system design, installation, and maintenance, ensuring that the conveyors operate at their best.
5. Dorner Mfg. Corp.
Dorner Mfg. Corp. is a leading manufacturer of precision conveyor systems, including packing conveyors. The company has been in business for over 50 years and has a deep understanding of the conveyor industry.
Features in Packing Conveyors:
- Light - Duty to Heavy - Duty Solutions: Dorner offers a wide range of packing conveyors, from light - duty conveyors for small parts handling to heavy - duty conveyors for large and heavy packages. Their conveyors can be customized to meet the specific load - carrying requirements of different applications.
- Sanitary Design Options: In industries such as food, pharmaceutical, and electronics, where cleanliness is crucial, Dorner provides conveyors with sanitary design options. These conveyors are easy to clean and can prevent the accumulation of dirt and debris, ensuring compliance with strict hygiene standards.
- Quick - Change Components: Dorner's conveyors feature quick - change components, which allows for easy maintenance and replacement. This reduces downtime and increases the overall efficiency of the packaging line. For example, the belts can be quickly replaced without the need for complex tools or procedures.
Advantages:
- Customer - Centric Approach: Dorner has a strong customer - centric approach. They work closely with customers to understand their needs and provide customized solutions. Their sales and support teams are responsive and dedicated to ensuring customer satisfaction.
- Innovation in Conveyor Design: The company is constantly innovating in conveyor design. They introduce new features and technologies to improve the performance and functionality of their packing conveyors. For example, they have developed conveyors with improved tracking systems to ensure accurate product movement.
- Training and Education: Dorner provides training and education programs for its customers. These programs help customers to better understand and operate their conveyors, and also provide them with the knowledge and skills to perform basic maintenance tasks.
6. FlexLink
FlexLink is a global provider of flexible conveyor systems for the manufacturing and packaging industries. The company focuses on providing solutions that can adapt to the changing needs of production processes.
Features in Packing Conveyors:
- Flexible Configuration: FlexLink's packing conveyors are highly flexible in configuration. They can be easily adjusted to different lengths, widths, and heights, and can also be combined with other conveyor sections to form complex conveyor systems. This flexibility allows for easy integration into existing production lines and adaptation to different product flow requirements.
- Low - Maintenance Design: The conveyors are designed for low - maintenance operation. They use durable components and simple mechanical designs, which reduces the need for frequent maintenance and replacement parts. This results in lower operating costs for customers.
- Product Protection: FlexLink's conveyors are designed to protect the products being transported. They use gentle handling techniques and smooth conveyor surfaces to prevent product damage during the packaging process. For example, in the electronics industry, where products are sensitive to shock and vibration, FlexLink's conveyors can ensure safe and reliable transportation.
Advantages:
- Industry Experience: FlexLink has extensive industry experience in providing conveyor solutions for various industries, such as automotive, food, and consumer goods. This experience allows them to understand the specific requirements of different industries and provide tailored solutions.
- Global Network: The company has a global network of sales and service offices. This enables them to provide local support to customers around the world, ensuring quick response times and efficient service.
- Sustainable Solutions: FlexLink is committed to providing sustainable solutions. Their conveyors are designed to be energy - efficient and use environmentally friendly materials, which helps customers to reduce their environmental impact.
7. Interroll Group
Interroll Group is a leading global provider of material handling solutions, including packing conveyors. The company is known for its innovative products and high - quality components.
Features in Packing Conveyors:
- Energy - Saving Rollers: Interroll's packing conveyors use energy - saving rollers. These rollers are designed to reduce friction and power consumption, resulting in significant energy savings over the long term. The company's rollers are also highly durable and require minimal maintenance.
- Modular and Scalable Design: The conveyors have a modular and scalable design, which allows for easy expansion and modification of the conveyor system. Customers can start with a basic conveyor configuration and add more modules as their production needs grow. This makes the conveyors a cost - effective solution for businesses of all sizes.
- Advanced Control Systems: Interroll's packing conveyors are equipped with advanced control systems. These systems can optimize the operation of the conveyors, such as adjusting the speed and flow of products based on the real - time production situation. This improves the overall efficiency of the packaging line.
Advantages:
- Technology Leadership: Interroll is at the forefront of technology in the material handling industry. They continuously invest in research and development to introduce new and improved products. Their technology leadership allows them to offer cutting - edge packing conveyor solutions to their customers.
- Global Presence: The company has a global presence, with manufacturing facilities and sales offices in many countries. This enables them to provide local support and quick delivery of products to customers around the world.
- Comprehensive Product Range: Interroll offers a comprehensive product range of packing conveyors and related components. Customers can find all the necessary parts and accessories for their conveyor systems from a single source, which simplifies the procurement process.
8. JLS Automation
JLS Automation is a leading provider of automated packaging solutions, including packing conveyors, for the food, medical, and consumer products industries. The company focuses on providing customized and integrated solutions to meet the specific needs of its customers.
Features in Packing Conveyors:
- Food - Grade Conveyors: In the food industry, JLS Automation offers food - grade packing conveyors. These conveyors are made of materials that are safe for food contact and are designed to meet the strict hygiene and safety standards of the food industry. They are easy to clean and can prevent cross - contamination.
- Integration with Packaging Equipment: JLS Automation's packing conveyors can be easily integrated with other packaging equipment, such as filling machines, sealing machines, and labeling machines. This allows for a seamless and efficient packaging process. For example, the conveyors can transfer products from the filling station to the sealing station without any interruption.
- Vision - Guided Conveyor Systems: The company uses vision - guided conveyor systems in some of its packing conveyors. These systems use cameras and sensors to detect the position and orientation of products on the conveyor, and can adjust the movement of the conveyor accordingly. This ensures accurate product placement and improves the quality of the packaging.
Advantages:
- Industry - Specific Expertise: JLS Automation has in - depth industry - specific expertise in the food, medical, and consumer products industries. They understand the unique requirements and challenges of these industries and can provide tailored packing conveyor solutions.
- Customization Capabilities: The company has strong customization capabilities. They can design and build packing conveyors according to the specific needs and specifications of each customer. This allows customers to get a conveyor system that is perfectly suited to their production processes.
- After - sales Support: JLS Automation provides excellent after - sales support. Their service team can provide training, maintenance, and technical support to ensure the long - term reliable operation of the packing conveyors.
9. KUKA AG
KUKA AG is a well - known global provider of automation solutions, including packing conveyors. The company is famous for its robotic technology and has a wide range of applications in the manufacturing and packaging industries.
Features in Packing Conveyors:
- Robotic Integration: KUKA's packing conveyors can be easily integrated with its robotic systems. Robots can be used to pick, place, and pack products on the conveyors, which increases the flexibility and efficiency of the packaging process. For example, in a high - volume production line, robots can work in tandem with the conveyors to handle products at a high speed.
- High - Precision Movement: The conveyors are designed for high - precision movement. They can accurately position products for further processing or packaging. KUKA uses advanced control systems and servo motors to ensure smooth and precise movement of the conveyors.
- Safety Features: KUKA places a high emphasis on safety in its packing conveyors. The conveyors are equipped with various safety features, such as emergency stop buttons, safety guards, and sensors. These features ensure the safety of operators and prevent accidents in the workplace.
Advantages:
- Robotic Expertise: KUKA's expertise in robotic technology gives it an edge in the packing conveyor market. The integration of robots with conveyors allows for more advanced and flexible packaging solutions.
- Global Service Network: The company has a global service network, which can provide timely support to customers around the world. Their service technicians are highly trained and can quickly resolve any issues with the packing conveyors.
- Innovation and R & D: KUKA invests heavily in research and development. They are constantly exploring new technologies and applications in the field of automation, which allows them to offer state - of - the - art packing conveyor solutions.
10. SSI Schaefer
SSI Schaefer is a global leader in intralogistics solutions, including packing conveyors. The company has a long history of providing comprehensive material handling solutions for various industries, such as logistics, e - commerce, and manufacturing.
Features in Packing Conveyors:
- High - Capacity Conveyors: SSI Schaefer's packing conveyors are designed for high - capacity operation. They can handle a large volume of products in a short period of time, which is suitable for industries with high - throughput requirements. The company uses advanced conveyor designs and high - power drive systems to achieve high - capacity performance.
- System Optimization: The company focuses on system optimization in the design of its packing conveyors. They analyze the entire material handling process and design the conveyors to fit seamlessly into the overall system. This ensures the efficient flow of products through the packaging line and reduces bottlenecks.
- Warehouse Integration: SSI Schaefer's packing conveyors can be easily integrated with warehouse management systems. This allows for real - time tracking of products and efficient inventory management. For example, the conveyors can be connected to the warehouse management software, which can monitor the movement of products on the conveyors and adjust the storage and retrieval processes accordingly.
Advantages:
- Comprehensive Solution Provider: SSI Schaefer is a comprehensive solution provider. They can offer not only packing conveyors but also a full range of intralogistics solutions, including storage systems, sorting systems, and software. This allows customers to get a one - stop solution for their material handling needs.
- Project Management Expertise: The company has strong project management expertise. They can manage large - scale projects from planning to implementation, ensuring that the packing conveyor systems are delivered on time and within budget.
- Global Experience: SSI Schaefer has global experience in providing intralogistics solutions. They have completed many projects in different countries and regions, and have a deep understanding of the local market requirements and regulations.
Conclusion
The top 10 packing conveyor manufacturers in the world, including Sunrise (Tianjin) Packaging Machinery Co., Ltd., Dematic, Intelligrated, Bosch Rexroth, Dorner Mfg. Corp., FlexLink, Interroll Group, JLS Automation, KUKA AG, and SSI Schaefer, each have their own unique features and advantages. These manufacturers offer a wide range of packing conveyor solutions, from simple and cost - effective systems to highly advanced and automated ones.
Sunrise (Tianjin) Packaging Machinery Co., Ltd. stands out for its cost - effectiveness, customization, and excellent after - sales service, making it a great choice for small and medium - sized enterprises. On the other hand, companies like Dematic and KUKA AG are known for their advanced technology and automation capabilities, which are suitable for large - scale and high - tech production environments.
When choosing a packing conveyor manufacturer, customers should consider their specific requirements, such as the type of products to be transported, the production volume, the available space, and the budget. By carefully evaluating the features and advantages of each manufacturer, customers can select the most suitable packing conveyor system to improve the efficiency and productivity of their packaging processes. Overall, the global packing conveyor market is highly competitive, and these top manufacturers are constantly innovating and improving their products to meet the evolving needs of the industries.
Send Inquiry